Forged Bars / SST
Seamless Steel Tubes
Seamless steel tubes in a wide range from 21.3x3mm to 660x100mm, compliant with EN 10297-1 standard. High-performance solutions for hydraulic cylinders, pressure vessels, and petrochemical reactors.
Technical Specifications
Key Features
- Superior pressure resistance with seamless production
- Homogeneous wall thickness distribution
- Wide size range (21.3 - 660mm outside diameter)
- Wall thickness up to 100mm
- Hydrostatic test applied
- Full length UT and MPI inspection
- Heat treatment options (Q+T, N, A, SR)
- Controlled inner and outer surface quality
Applications
- Hydraulic cylinder bodies
- Pressure vessels and reactors
- Petrochemical process piping
- Power plant boiler tubes
- Offshore platform structural tubes
- Mining transmission lines
- Defense industry applications
- Shipbuilding and marine
Dimension Table
| Dimension (mm) | Length (m) | Weight (kg/m) | Tolerance (mm) | Standard |
|---|---|---|---|---|
| 21.3 x 3 | 3 - 12 | 1.35 | +/-12.5% | EN 10297-1 |
| 33.7 x 4 | 3 - 12 | 2.93 | +/-12.5% | EN 10297-1 |
| 60.3 x 5 | 3 - 12 | 6.82 | +/-12.5% | EN 10297-1 |
| 88.9 x 6.3 | 3 - 12 | 12.84 | +/-12.5% | EN 10297-1 |
| 114.3 x 8 | 3 - 12 | 20.99 | +/-12.5% | EN 10297-1 |
| 168.3 x 10 | 3 - 12 | 39.01 | +/-12.5% | EN 10297-1 |
| 219.1 x 12.5 | 3 - 12 | 63.67 | +/-10% | EN 10297-1 |
| 273 x 16 | 3 - 12 | 101.4 | +/-10% | EN 10297-1 |
| 323.9 x 20 | 3 - 12 | 149.9 | +/-10% | EN 10297-1 |
| 406.4 x 25 | 3 - 12 | 235.1 | +/-10% | EN 10297-1 |
| 508 x 40 | 3 - 10 | 461.6 | +/-10% | EN 10297-1 |
| 660 x 100 | 3 - 8 | 1381.0 | +/-10% | EN 10297-1 |
Technical Notes
- 01Wall thickness tolerances are applied per EN 10297-1 Table 8.
- 02Hydrostatic test pressure is calculated per standard requirements.
- 03Minimum order quantity applies for large diameter tubes (>323.9mm).
- 04Inner surface quality can be honed for hydraulic cylinder applications.
- 05Consult for special steel grades (low temperature, corrosion resistance).
- 06Pipe ends can be delivered as plain cut, beveled, or threaded.
Other Types
What is a forged bar?
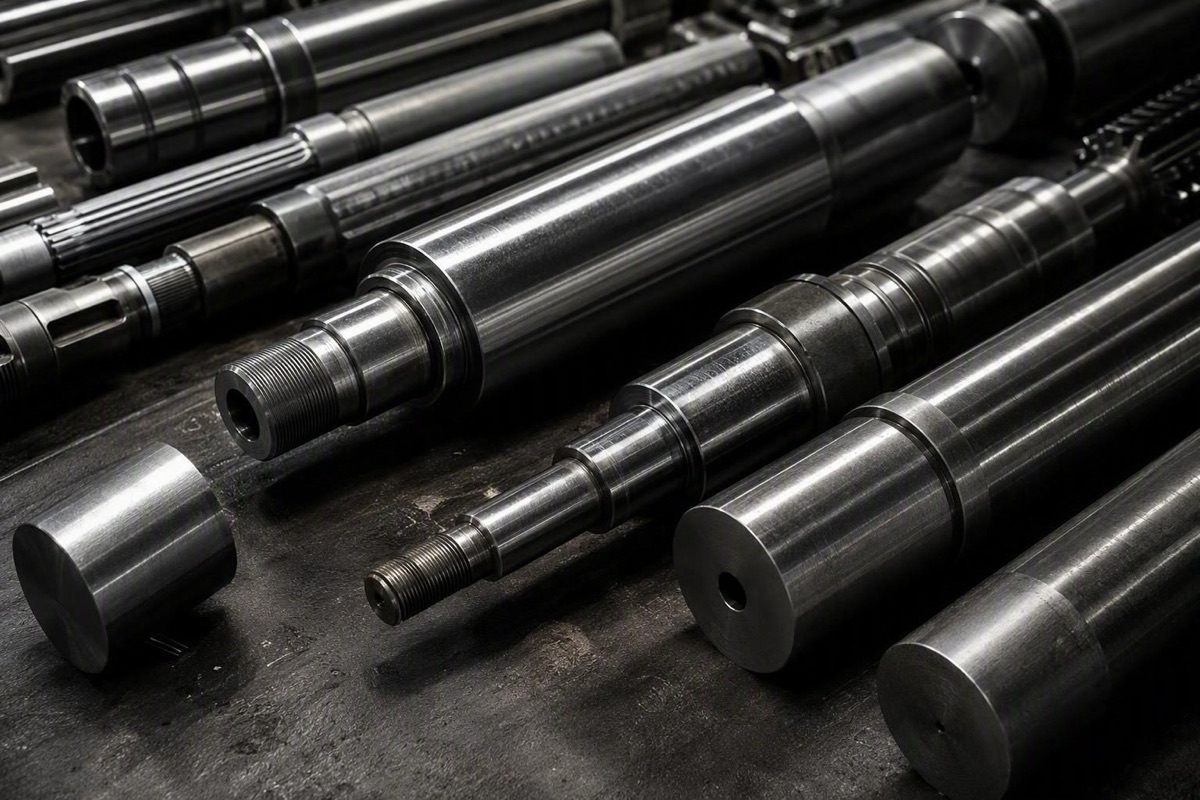
A forged bar is produced by pressing or hammering steel above its recrystallization temperature (~1100–1250°C). Forging closes internal voids and casting porosity, aligns the grain flow with the part geometry, and gives higher toughness, fatigue strength and internal soundness than rolled product. It is preferred for large-diameter shafts, gear blanks and critical machine parts.
Open-die forging, reduction ratio and quality assurance
In open-die forging, the material is progressively drawn out and rotated under a press; a reduction ratio of at least 3:1 is typically specified — it breaks up the ingot structure and homogenizes mechanical properties. Forgings are then normalized or quenched and tempered. Internal soundness is verified by ultrasonic testing (EN 10228 / SEP 1921). Q&T grades such as 42CrMo4, C45 and 34CrNiMo6 are the most common forged qualities; diameters beyond rolling capacity (Ø200 mm+) can only be produced by forging.
Frequently Asked Questions
Forged bar vs rolled bar — what is the difference?+
Forging closes internal porosity and aligns grain flow, giving higher toughness and fatigue strength in the same grade. Rolling is faster and cheaper; forging is chosen for large diameters and critical parts.
Why does the reduction ratio matter?+
A ratio of at least 3:1 breaks up ingot segregation and voids, guaranteeing a homogeneous, sound core. Critical specifications state it explicitly.
Which grades are supplied as forged bar?+
Most commonly Q&T steels such as 42CrMo4, C45, 34CrNiMo6 and 36CrNiMo4, plus tool steels and large-section carbon steels.
How are forged bars tested?+
Ultrasonic testing (EN 10228/SEP 1921) verifies internal soundness; chemistry and mechanical tests are reported in the EN 10204 3.1 certificate.
Related Blog Posts
Technical articles, guides and industry analyses
C45 vs 42CrMo4 Steel: Carbon or Alloy — Which to Choose?
We compare C45 (1045) carbon steel with 42CrMo4 (4140) chrome-moly quenched & tempered steel by hardenability, strength, welding and cost — which to choose and when?
Quenched and Tempered Steels: EN 10083 Grades, Values and How to Choose
Quenched and tempered (Q&T) steel is the class that delivers strength and toughness together. We put the six main EN 10083 grades — C45, 25CrMo4, 42CrMo4, 39NiCrMo3, 34CrNiMo6, 51CrV4 — into one table with chemistry, section-dependent values and selection criteria.